Reject Confirmation
Evidence that the suspect pack actually left the line
A Reject Command Is Not Proof of Removal
A detection decision is information. It becomes control only when the suspect pack is physically removed from the accepted product flow and kept away from it.
Without reject confirmation or equivalent independent evidence, an inspection record may show only that a reject was commanded, not that the pack reached the reject bin. That gap stays invisible until someone asks for the evidence.
Where Rejection Fails in Practice
- The reject device fires, but the pack stays on the belt, for example because of reject timing at higher line speeds
- The reject bin is full and quietly stops isolating anything
- Air pressure drops, so an air reject no longer removes the pack reliably
- A shared or unsecured reject area, where rejected product can find its way back into the accepted flow
- No defined response when a rejection cannot be confirmed
The system triggers the reject device, but nothing checks whether the pack actually reached the reject bin
Sensors check each rejection, and the system stops with a clear message when a pack does not reach the bin
How Reject Confirmation Works on MEKI ONE
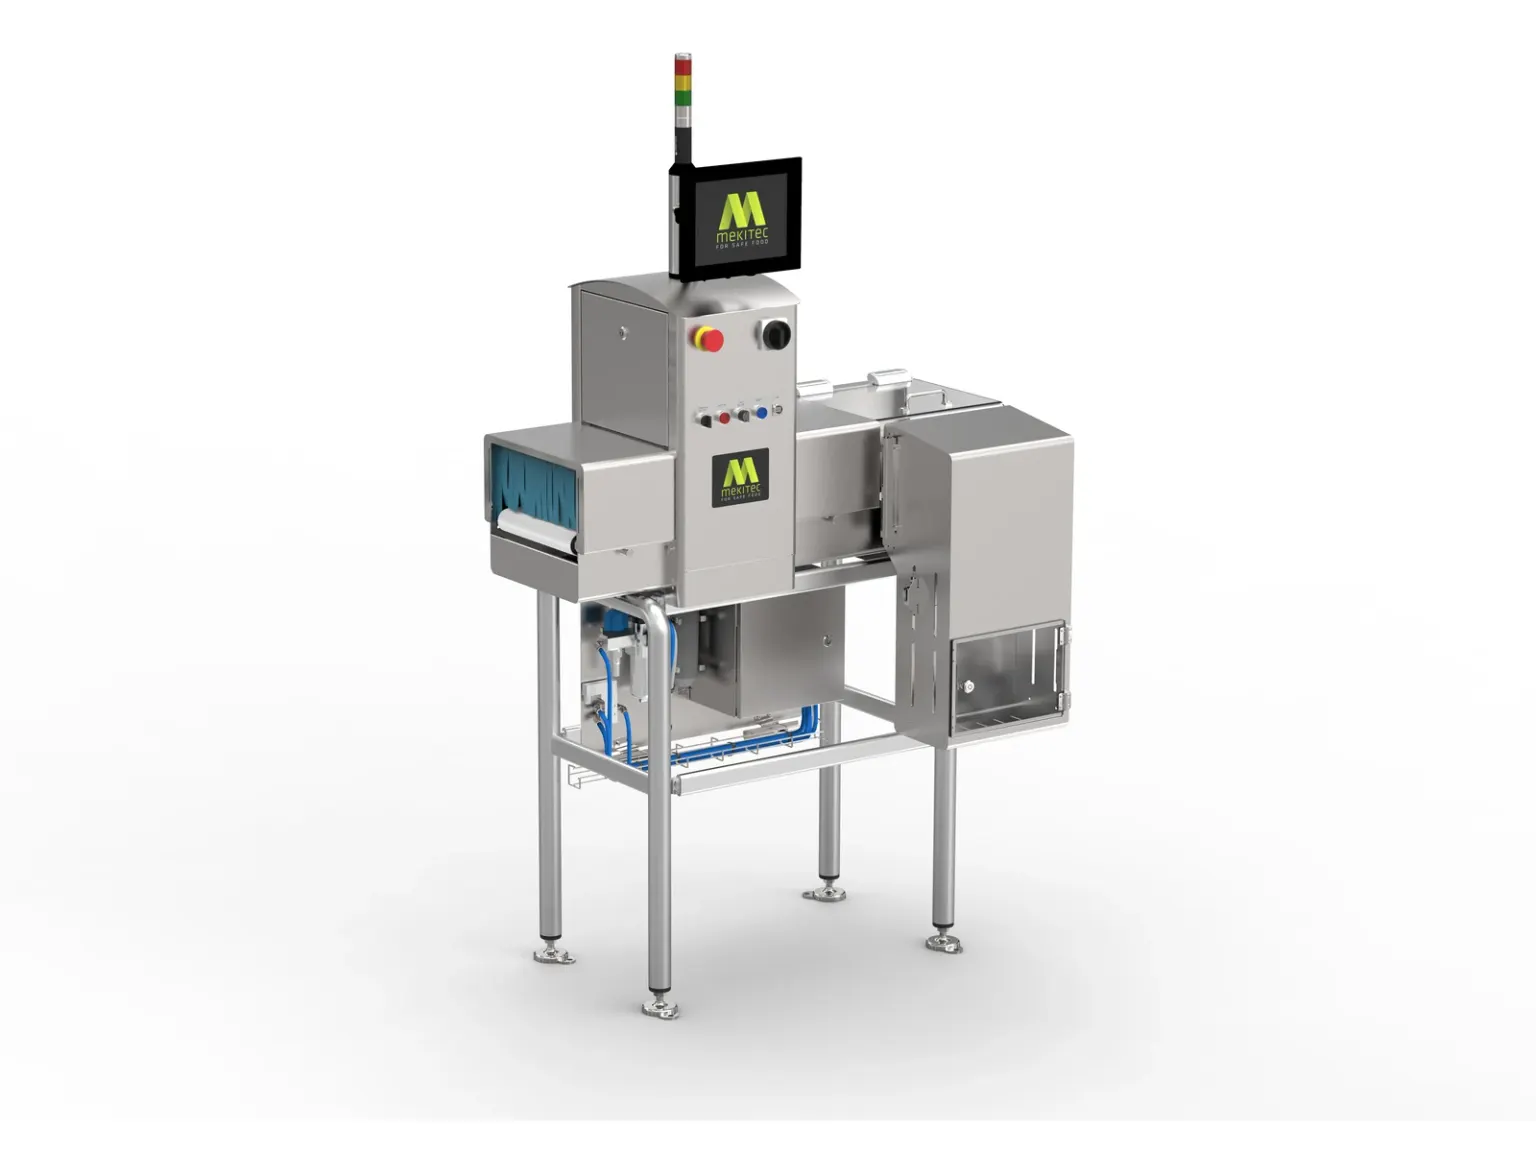
Every MEKI ONE comes with the standard reject confirmation kit, integrated into the frame together with the air reject and the reject bin. It monitors:
- Each rejection: a rejected pack must pass the light curtain sensors at the opening of the reject bin
- Reject bin full: a sensor detects when the bin is full
- Reject bin almost full: a warning tells operators to empty the bin before it becomes a stop
- Air pressure: the system's air pressure, which the air reject depends on, is monitored against an adjustable limit
When a pack does not reach the bin, the bin is full or the air pressure is too low, the system stops and an error message on the screen states the reason, with a blinking blue light on the light tower. Depending on the settings, the X-ray generator and the conveyors stop, or only a short reject conveyor. Once the cause is removed, for example by emptying the bin, the operator acknowledges the message with the reset button.
Full reject confirmation is available for MEKI ONE as an option.
Other MEKI Systems
On other packaged-product systems, the reject system is selected for the product, the package and the line layout:
- Air, pusher, flipper and drop-down rejection, with one or two reject systems
- Reject confirmation can be added to the reject system, for example on MIDMEKI, and is configured for the application
What Reject Confirmation Proves, and What It Does Not
Reject confirmation provides evidence that the monitored point in the reject sequence was reached: here, that the rejected pack passed the sensors at the opening of the reject bin. What it proves depends on sensor placement and logic, so the supplied configuration is confirmed for each application.
It does not replace control of the reject bin and its contents, the decision on what happens to rejected product, or your site's defined response to a failed rejection. A CCP validation challenges both detection and the removal of the suspect pack under production conditions.
Part of a Complete X-ray CCP
A Critical Control Point for foreign bodies has to answer five questions. Reject confirmation answers the second and the third:
- INSPECT: Was the product inspected? See foreign object detection at the CCP.
- REMOVE and PROVE: Was suspect product removed, and was removal confirmed? See reject confirmation (this page).
- CHECK: Were the routine checks done? See Validation Mode.
- RECORD: Can the records be retrieved for a defined line, product and time window? See CCP Monitoring and reject records with X-ray images.
Equipment and software support the CCP. Validating it for each product remains part of your site's procedures. Read more in What Makes a Critical Control Point Complete?
Plan Removal Together With Inspection
Define the reject configuration together with the inspection, so that testing and validation cover the whole sequence from detection to the reject bin.
Discuss Your Reject Configuration
Disclaimer: All information is provided for information purposes only and shall not be considered as assured characteristics. The information and technical data presented in this document are subject to change. Customers should obtain and verify the latest relevant information before placing orders.
Key Features
Sensors at the Bin Opening
Each rejected pack must pass the light curtain sensors at the reject bin
Bin Full and Almost Full
A warning when the bin is almost full and a stop when it is full
Air Pressure Monitoring
The system's air pressure is monitored against an adjustable limit
Clear Stop Messages
The screen states the reason for each stop, with a blue signal on the light tower